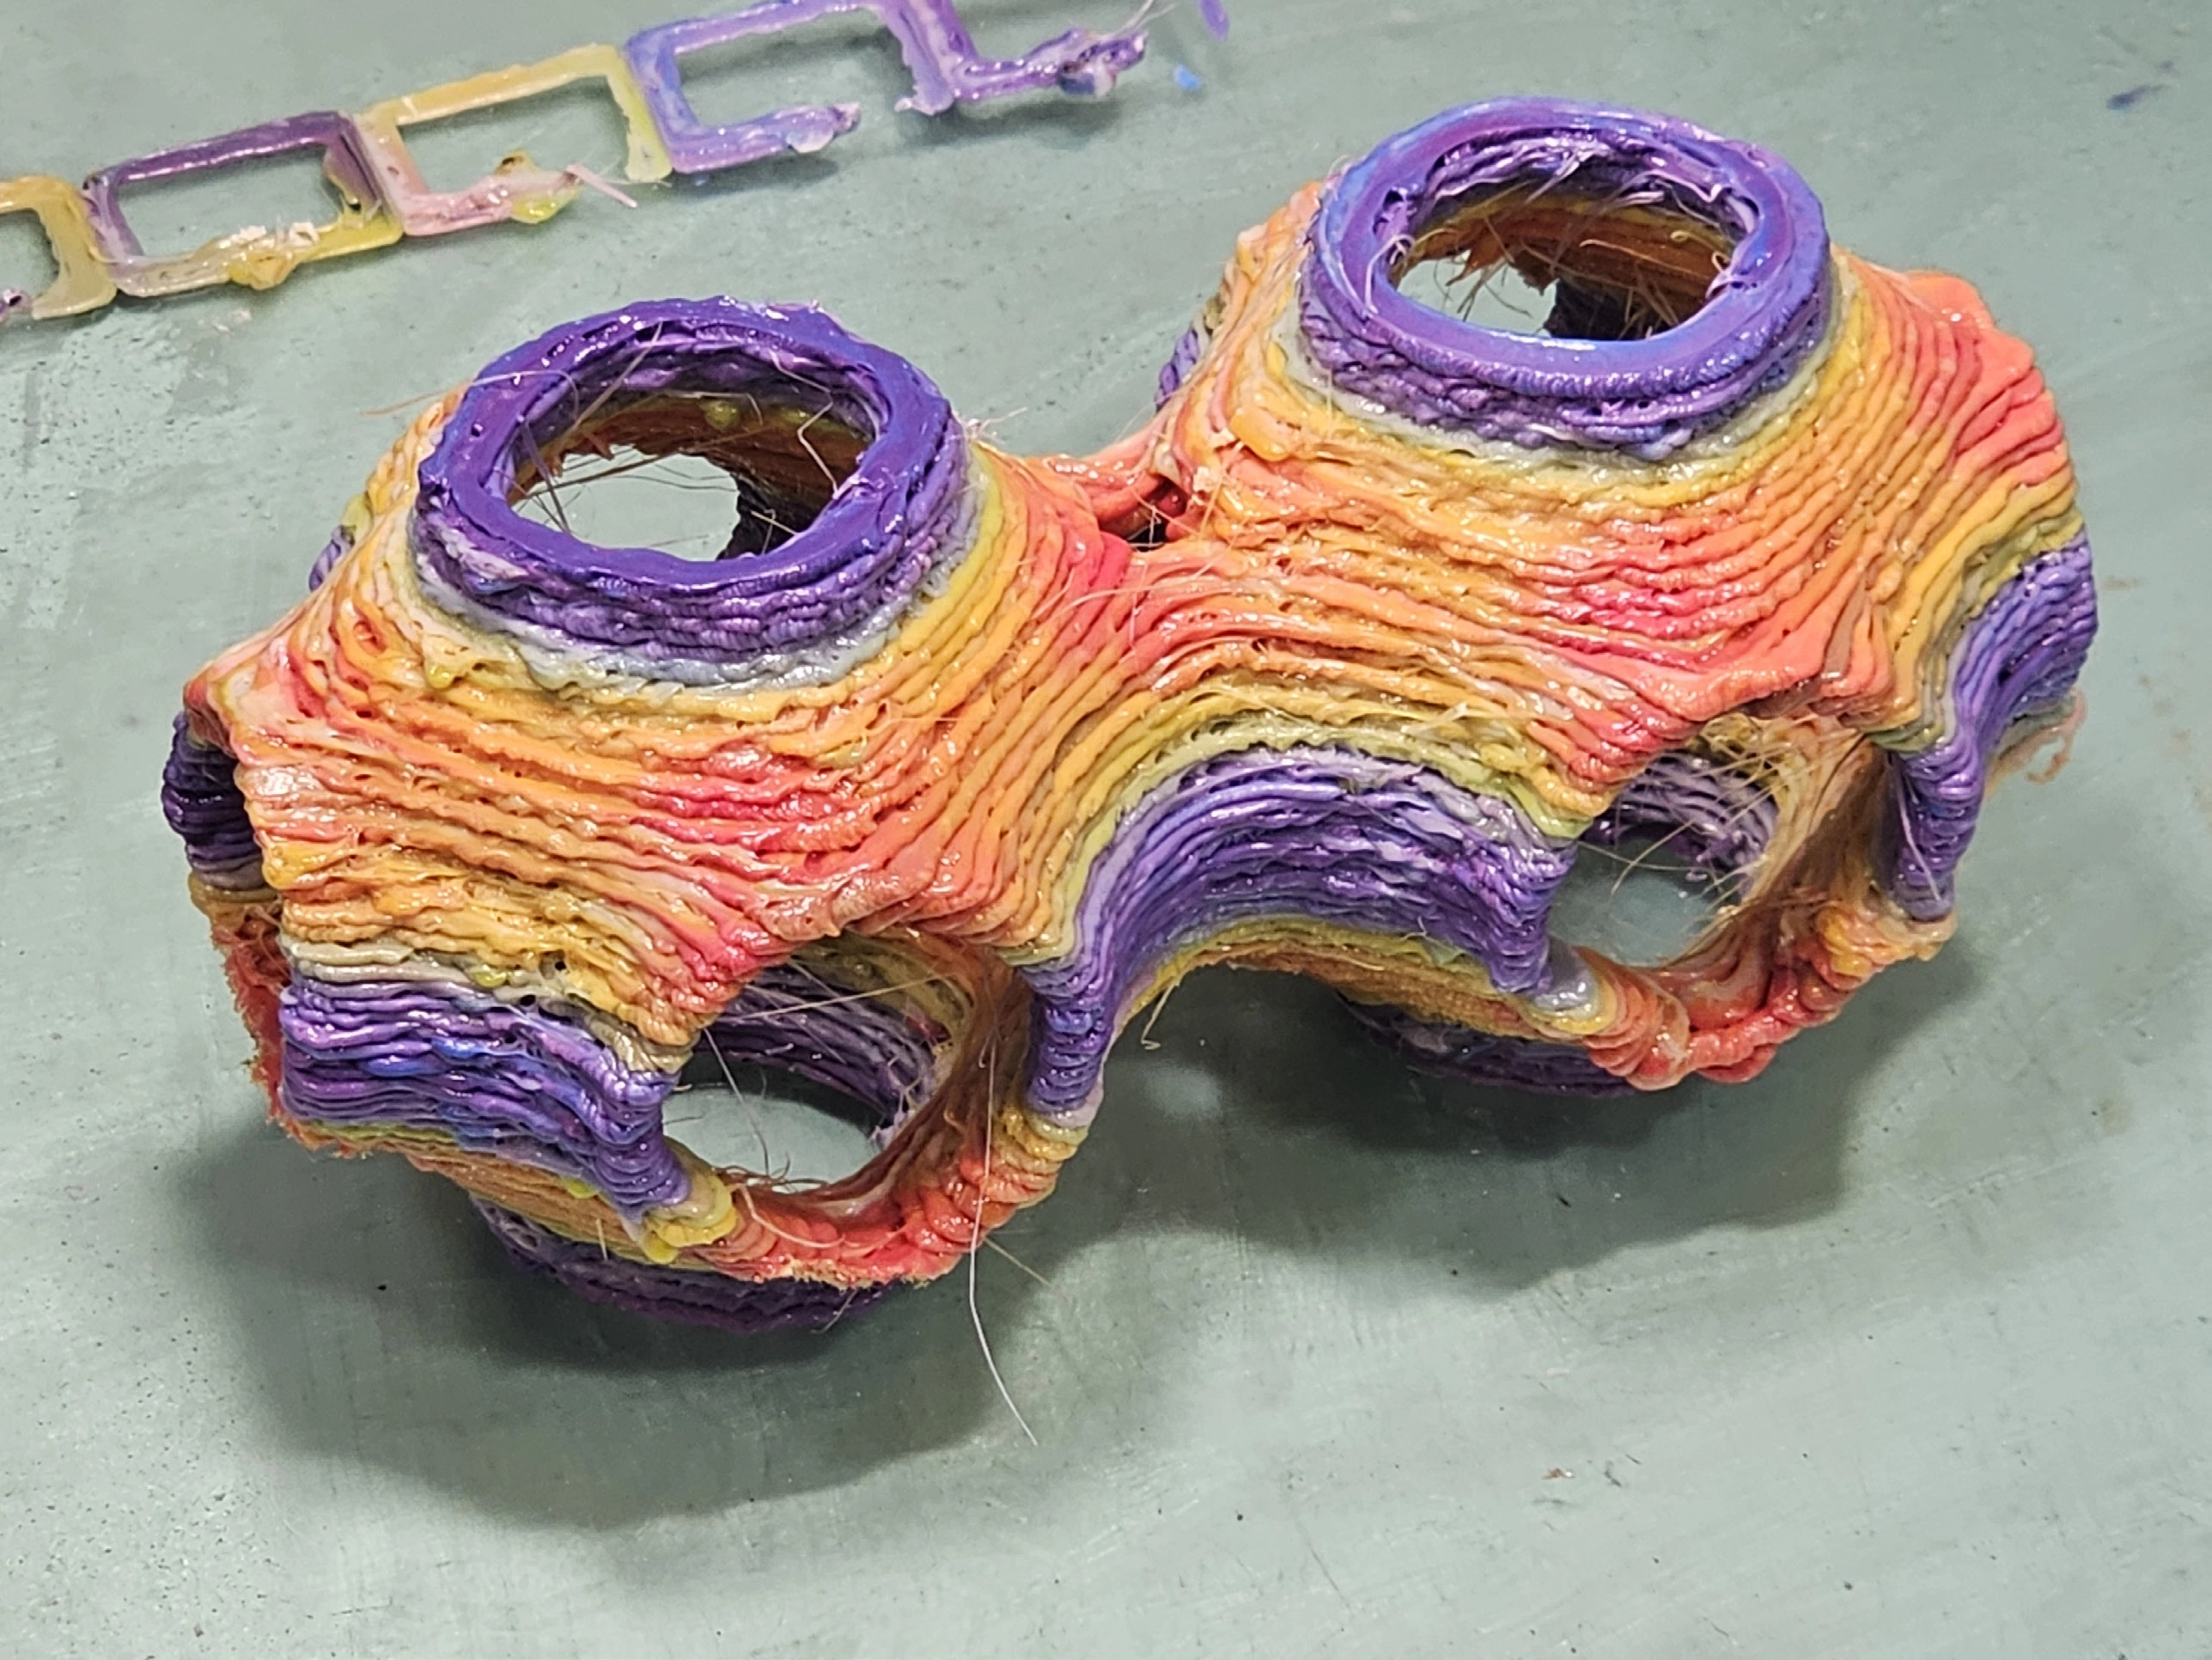
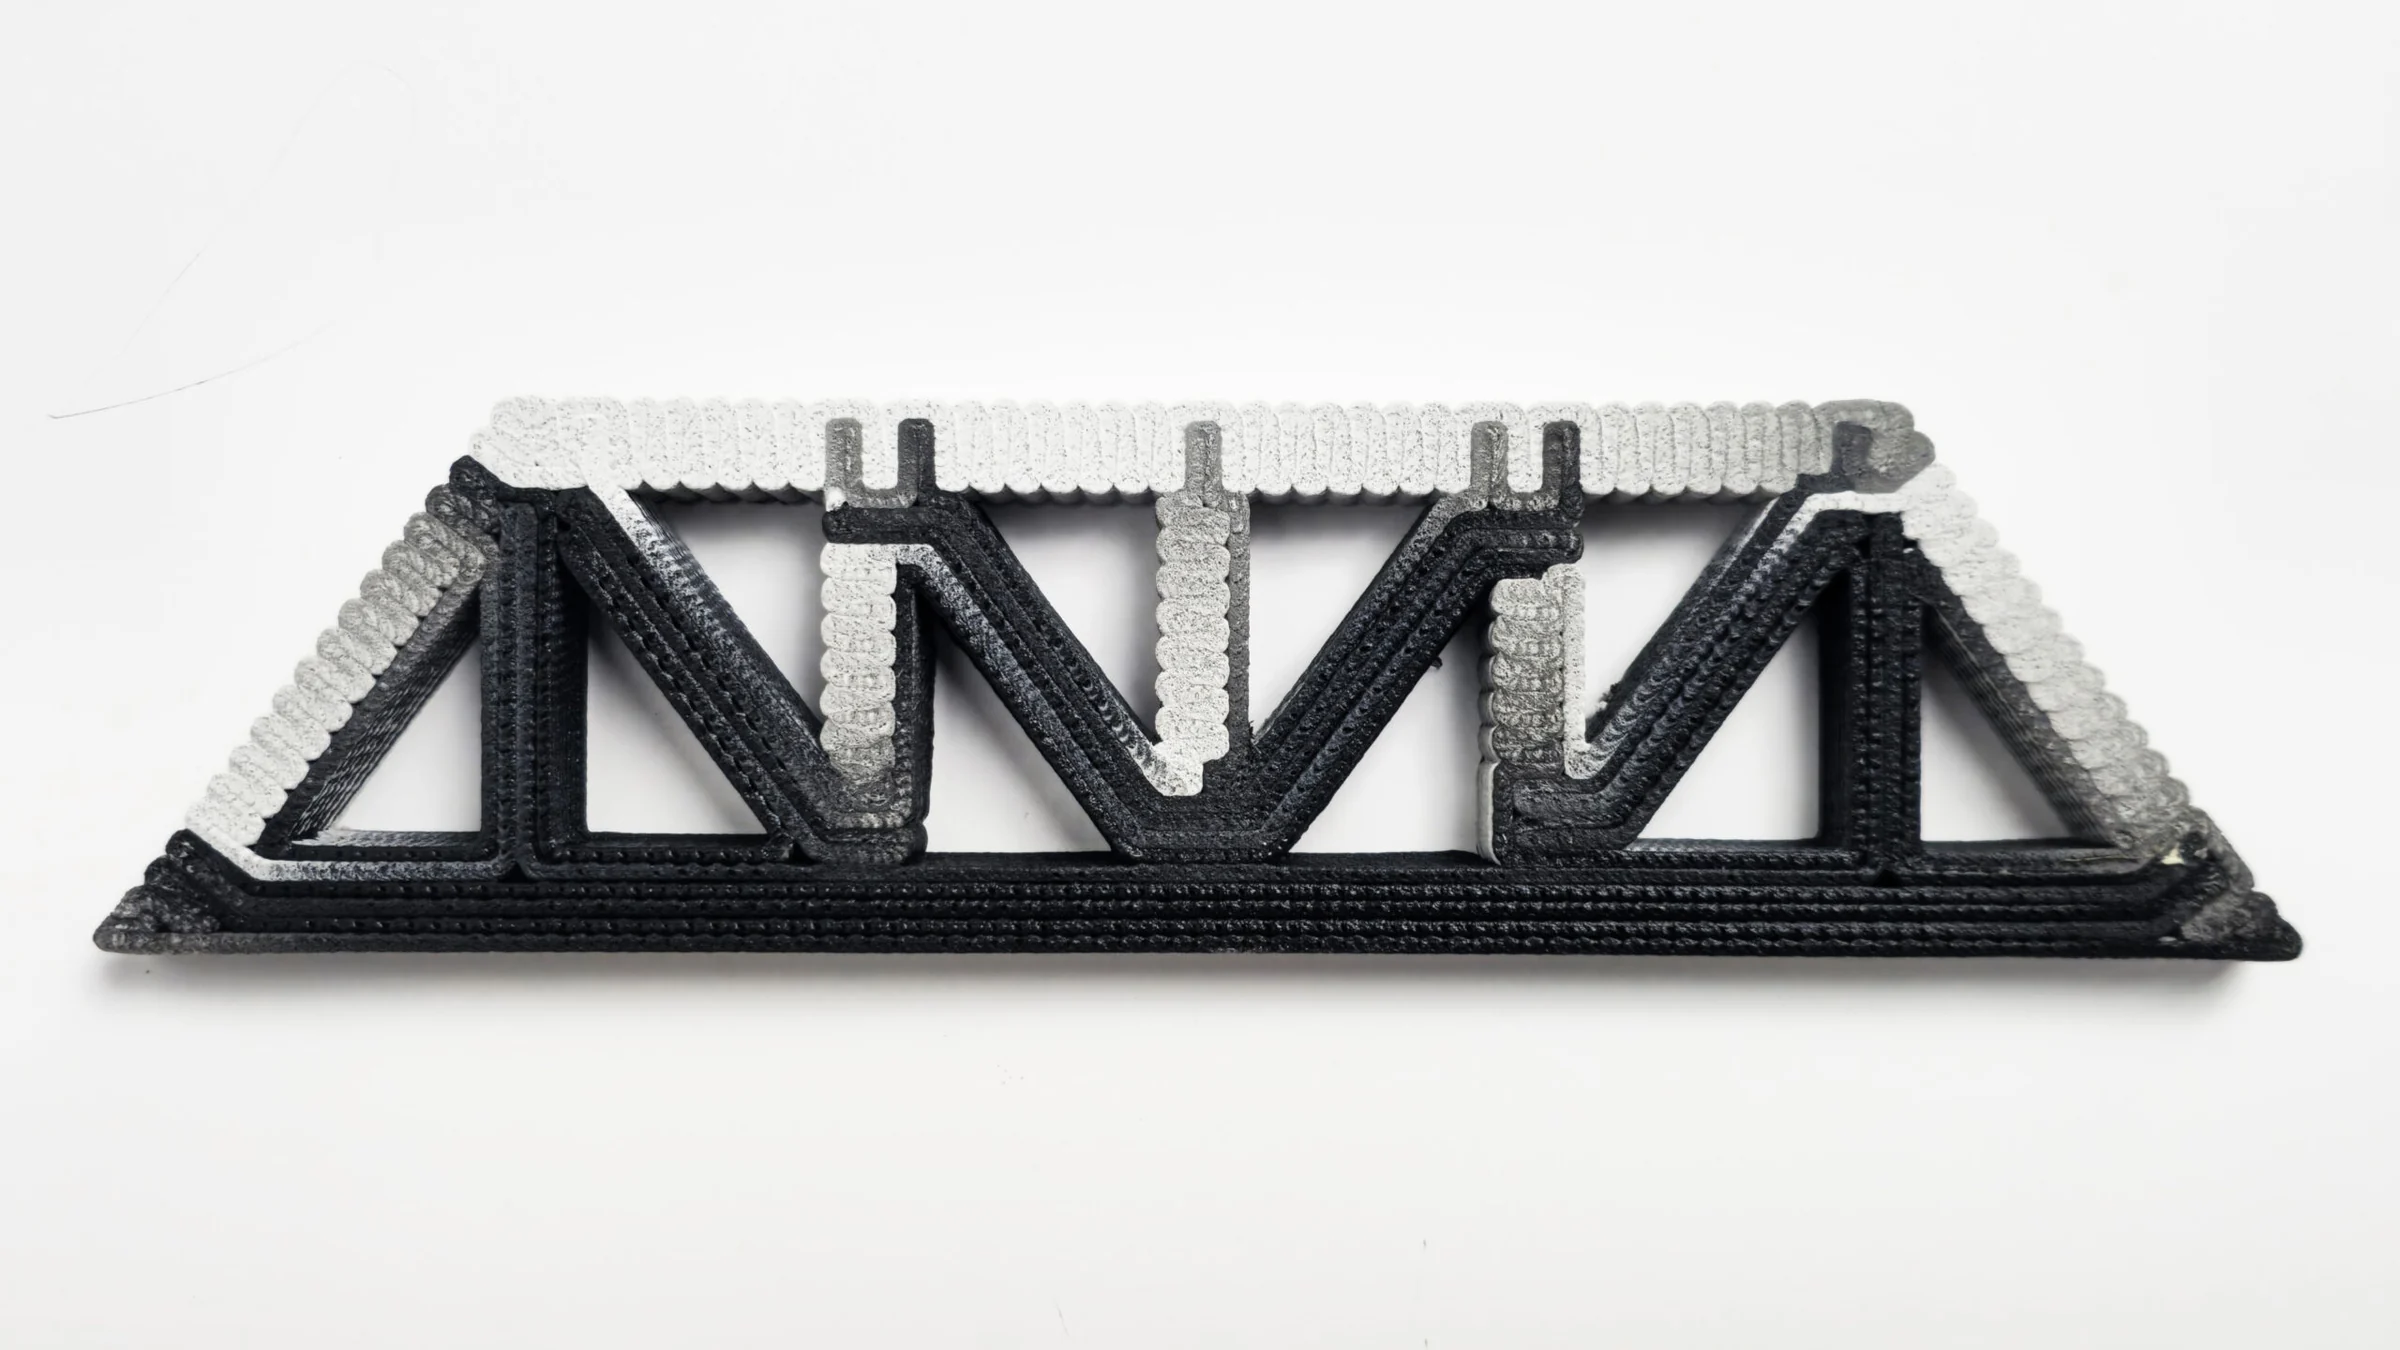
Printed graded footwear, material-transition studies, and deposition video demonstrate the workflow. Simulated loading informs placement; wearer performance is not established here. View evidence ↓
Printing the graded sneaker
The US men’s size 10 sneaker combines five material formulations in a single print. Blue PET-G makes the composition changes visible across the sole, toe, sidewall, and upper. The prototype is reported at 350 g, with 45 minutes of continuous extrusion per sneaker and no support material or post-assembly.
Continuous fabrication of the sneaker (left) and a close view of deposition around the toe (right).
Continuous multi-material deposition
Printing the footwear prototype with continuous variation in material composition.
Simulated stress and the corresponding printed material regions across the toe and upper.
Side view comparing the simulated response with the composition gradient in the printed shoe.
Material composition follows the body
The heel, arch, forefoot, and upper experience different combinations of compression, bending, and contact. This project assigns local material mixtures to those demands, producing a shoe whose composition changes continuously between flexible and supportive regions. Recycled TPU and PET-G form the thermoplastic feedstocks; polyol additives adjust the TPU blend before it is combined with PET-G.
A single nozzle with active mixing deposits the graded material as one body. The resulting prototypes integrate upper and sole without stitching or adhesive joints, linking functional zoning directly to the fabrication sequence.
Two-stage mixing head with independently controlled thermoplastic and additive feeds (left); functional material regions within the shoe (right).
From simulated loading to material zones
Finite element analysis examines loading during heel strike, mid-stance, and toe-off. Stress and deformation patterns inform surface regions with different composition targets: PET-G-rich blends reinforce the toe and ground-contact zones, while softer TPU-rich blends accommodate bending and fit around the upper.
The simulation guides where properties are assigned; printed specimens show how those assignments are materialized.
Shoe geometry, finite element simulation, and the resulting material-zone model.
Programming softness and the transition
Four controlled feeds enter a two-stage mixing chamber. Recycled TPU first mixes with polyether and polyester polyols; the adjusted blend then mixes with PET-G before extrusion. Feed rates define composition, while auger rotation affects how material transitions develop along the deposited path.
The material study reports Shore 62A–93A across the tested polyol formulations. Separate transition samples and tensile strips examine mixing speed: lower speeds produce longer gradients in the transition samples and higher peak stresses in the tested PET-G/TPU interfaces. These results connect the material boundary to a fabrication parameter that can be controlled during printing.
Color-transition samples at different auger speeds, a tensile specimen, and stress–strain curves for the tested PET-G/TPU interfaces.
Encoding mixtures along a continuous path
Closed material-zone geometries intersect the extrusion curves to assign each path segment a mixture. Eight cross-sections from toe to heel illustrate how these assignments change through the shoe. Material-change commands are advanced along the path by a calibrated distance to compensate for the material retained in the mixing chamber.
The exported G-code coordinates movement and feed ratios, allowing composition to vary without breaking the extrusion path or assembling separate material components.
Eight cross-sections from toe to heel show the local material assignments along the extrusion paths.
Adapting the gradient to different footwear
The sneaker places stiffer mixtures in selected sole and toe regions while retaining compliance through the upper. A US women’s size 8 flat uses a more TPU-rich distribution for a lower-profile form. Manual compression demonstrates localized flexibility in its forefoot and arch, extending the fabrication method to a second footwear geometry.
Stress-informed material distribution in the sneaker sole (left); the printed flat and manual compression of its forefoot and arch (right).
Circularity through feedstock and fabrication
Failed TPU and PET-G prints are shredded and returned to the extrusion feed. Integrating upper and sole removes adhesive joints and assembly operations from the demonstrated process. Long-term wear, user comfort, and recovery of the mixed polymers after use require further testing to establish the full lifecycle performance of the footwear.
Related publications
All publications →-
Accepted for ACADIA 2026 · Conference in October 2026
Embodied Material Gradients: Reframing 3D-Printed Footwear through Circular Multi-Material Fabrication